

2026 Top Folding Carton Packaging Types for Global Buyers?
In 2026, global buyers will examine folding carton packaging beyond color, shape, and shelf appeal. They will compare material performance, converting quality, compliance readiness, and total delivered cost. A carton may look elegant in a sample room, yet fail beside a humid loading dock. That detail matters.
Smithers’ The Future of Folding Cartons to 2028 identifies continued demand for cartons across food, healthcare, personal care, and household products. The report also highlights sustainability pressure, lightweighting, premium finishes, and improved print efficiency. Meanwhile, Pro Carton’s European market research shows how folding cartons remain important in branded consumer goods and retail presentation. These findings support a practical question: which carton format fits each product, channel, and region?
Not every “eco” claim survives a full supply-chain review. Buyers should check fiber sourcing, recycled content, coatings, inks, recyclability, barrier performance, and local recycling conditions. The Packaging Machinery Manufacturers Institute also reports stronger industry attention toward automation, flexible production, and packaging efficiency. Those trends influence carton choices, especially for companies managing multiple SKUs and shorter production runs.
This guide reviews the leading 2026 folding carton packaging types for global buyers. It connects structural design with product protection, visual merchandising, production speed, and transport realities. Expect familiar formats, but not identical results. A tuck-end carton can perform well for cosmetics, while a crash-lock base may suit heavier retail products. The right answer depends on evidence, testing, and honest supplier communication. Even this outlook has limits. Market forecasts change, and regional conditions can overturn a confident specification.
What Are Folding Cartons and Why Do Global Buyers Choose Them?
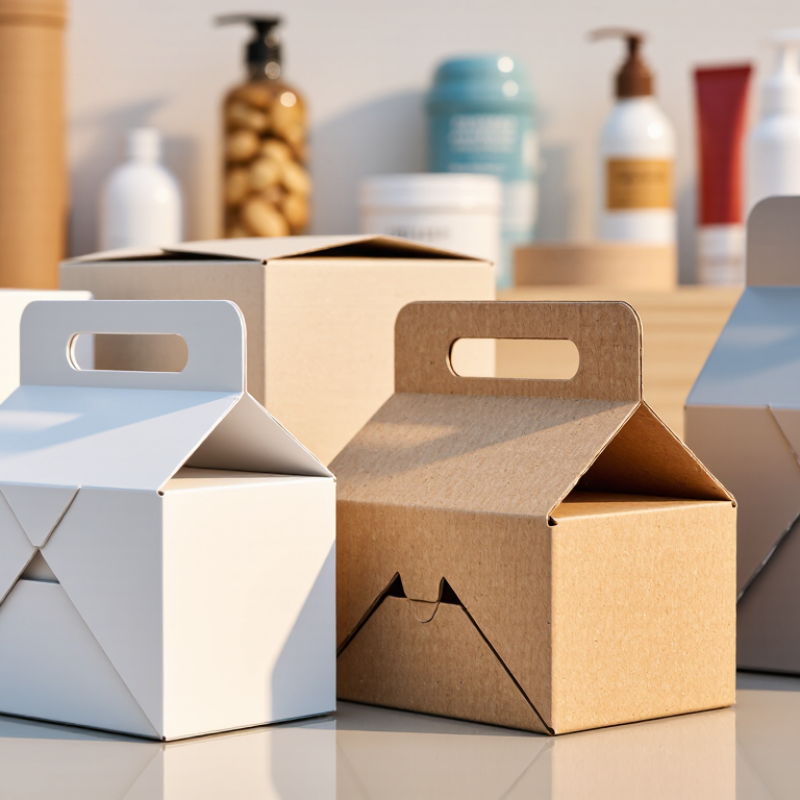
Folding cartons are paperboard boxes that are creased, printed, and delivered flat. Buyers form them during packing, reducing storage volume and transport costs. Common structures include tuck-end cartons, sleeve cartons, auto-lock boxes, and window cartons.
They are practical, not magical. Smithers’ 2024 market report, The Future of Folding Cartons to 2028, forecasts global demand to grow by about 4% annually through 2028. This growth reflects strong use in food, personal care, household, and pharmaceutical packaging. Folding cartons also support high-quality graphics, batch codes, tamper-evident features, and recyclable paper-based formats where local systems can process them. A small carton can carry a surprising amount of information.
Global buyers often choose them because specifications are easy to standardize. A purchaser can compare board thickness, folding style, print coverage, coating, and pack count across suppliers. The Paper and Paperboard Packaging Environmental Council reports that paper packaging recovery in the United States remains above 60%, although recovery rates differ widely by region. That difference matters. A recyclable carton is not automatically recycled everywhere.
In factory trials, buyers should check carton compression, crease accuracy, moisture resistance, and machine speed. A carton that looks perfect may split at the tuck flap. Humid warehouses expose weak designs quickly. Buyers sometimes overvalue appearance and undervalue filling performance. That is a costly mistake. Independent testing and documented material specifications make sourcing more reliable.
| Folding Carton Type | Typical Structural Features | Common Product Applications | Typical Paperboard Range | Flat-Pack and Shipping Efficiency | Opening and Assembly | Recyclability Considerations | Why Global Buyers Choose It |
|---|---|---|---|---|---|---|---|
| Straight Tuck End Carton | Top and bottom closure panels tuck in the same direction; clean front and side presentation. | Cosmetics, personal care, small electronics, health products, and retail accessories. | Typically 250–500 gsm, depending on product weight and required stiffness. | Very high Ships flat and uses warehouse space efficiently. |
Quick manual filling; suitable for automated cartoning lines with compatible dimensions. | Usually recyclable when made from paperboard with limited non-paper components. | Provides a neat retail appearance, reliable closure, and efficient production for standard product shapes. |
| Reverse Tuck End Carton | Top and bottom tuck flaps close in opposite directions; often reduces material overlap. | Pharmaceutical products, food supplements, household goods, and lightweight consumer products. | Typically 250–450 gsm. | Very high Flat-packed delivery lowers storage and freight volume. |
Easy to assemble manually; commonly compatible with high-speed packing equipment. | Paperboard structures are generally suitable for established paper recycling streams, subject to local rules. | Offers a cost-effective balance of material use, protection, and fast packing performance. |
| Auto-Lock Bottom Carton | Pre-glued locking base forms automatically when the carton is opened; top may use a tuck flap. | Bottles, jars, candles, heavier cosmetics, food containers, and premium retail products. | Typically 300–600 gsm. | High Delivered flat but requires more board than basic tuck-end styles. |
Fast setup with strong bottom support; reduces manual bottom folding during packing. | Recyclability is generally favorable if adhesives, coatings, and inserts are compatible with local recycling systems. | Improves packing speed and supports heavier products without separate plastic or foam bases. |
| Crash-Lock Bottom Carton | Pre-glued base locks into position when opened; designed for quick forming and enhanced load support. | Food trays, household products, beverage accessories, gift sets, and medium-weight packaged goods. | Typically 300–600 gsm. | High Flat shipment with efficient case packing after forming. |
Rapid automatic or semi-automatic setup; suitable for operations prioritizing labor efficiency. | Paper-based construction can support recyclability, but coatings and laminated layers should be reviewed. | Combines strong bottom performance with fast machine or manual assembly for international supply chains. |
| Sleeve Carton | Open-ended paperboard sleeve slides over a tray, box, pouch, or existing primary package. | Food trays, soap boxes, gift packaging, apparel accessories, and promotional multipacks. | Typically 250–450 gsm. | Excellent Simple die-cut format with low material volume and efficient nesting. |
Very easy to apply manually or by sleeve-applying equipment; usually does not require a full carton former. | Often recyclable when printed paperboard is used without difficult-to-separate materials. | Provides strong branding space while reducing board consumption compared with a fully enclosed carton. |
| Window Folding Carton | Folding carton fitted with a transparent viewing panel, usually made from a separate film or cellulose-based material. | Bakery items, toys, gift products, apparel accessories, cosmetics, and visible consumer goods. | Typically 300–500 gsm. | High Ships flat, although the window adds converting and material requirements. |
Usually supplied as a flat carton; may require manual or automated forming depending on the design. | Recyclability depends on the window material, adhesive, and local sorting rules; mono-material designs simplify recovery. | Allows product visibility while retaining the printable surface and protective structure of a carton. |
| One-Piece Tuck-Top Carton | Integrated body and lid with a tuck-in top; may include dust flaps or locking tabs. | Apparel, books, stationery, small gifts, electronics accessories, and subscription products. | Typically 300–600 gsm. | High Flat-packed and suitable for efficient parcel fulfillment. |
Simple folding and closing; convenient for repeated opening and closing. | Generally compatible with paper recycling when free from excessive plastic lamination or mixed-material components. | Offers a practical unboxing experience and can be adapted to many product dimensions. |
| Gable-Top Folding Carton | Folding structure with a peaked top and integrated handle or closure area. | Takeaway food, bakery products, confectionery, gifts, and small foodservice packages. | Typically 300–500 gsm; food-contact grades may be required. | Medium to high Efficient when flat, but the shaped top requires additional board area. |
Can be formed manually or by equipment; handle and top closure support convenient carrying. | Food-contact coatings and moisture barriers should be checked for compatibility with local recycling facilities. | Combines carrying convenience, shelf presence, and a paper-based alternative to some rigid plastic formats. |
| Hanger Carton | Includes an integrated or attached hanging tab for pegboard retail display. | Hardware, cables, small tools, toys, personal care items, and compact accessories. | Typically 300–500 gsm. | High Flat-packed and designed for efficient retail replenishment. |
Usually easy to erect; integrated tabs avoid separate display hardware. | Paperboard is generally recyclable; metal or plastic hanging components may require separate evaluation. | Supports vertical merchandising and improves product visibility in limited retail space. |
| Two-Piece Folding Carton | Separate lid and base, often with a tray-style interior and a close-fitting outer cover. | Premium gifts, jewelry, electronics accessories, chocolates, and presentation-focused products. | Typically 350–700 gsm, sometimes reinforced with additional paperboard layers. | Medium Requires more material and may occupy more assembled volume than tuck-end formats. |
Simple closing action and strong presentation; suitable for manual premium packing. | Recyclability depends on inserts, magnets, ribbons, foils, laminates, and other decorative additions. | Creates a premium unboxing experience and offers strong protection for higher-value products. |
| Display-Ready Folding Carton | Carton converts from a shipping or protective format into an in-store display tray with tear-away sections. | Fast-moving consumer goods, snacks, cosmetics, small household items, and promotional assortments. | Typically 350–650 gsm, depending on display load and transport requirements. | High Combines transport packaging and retail display functions. |
Designed for quick shelf placement with minimal unpacking labor. | Recyclability is generally favorable when tear strips, coatings, and adhesives remain paper-compatible. | Reduces store labor, limits secondary packaging, and supports consistent retail presentation across markets. |
Buyer note: Paperboard weights, dimensions, closure performance, coating selection, food-contact suitability, and recycling outcomes vary by product requirements, converting equipment, transport conditions, and destination-market regulations.
Technical basis: The ranges and characteristics above reflect commonly used folding-carton structures and commercial paperboard specifications. Final specifications should be confirmed through dieline testing, compression testing, transit testing, and local packaging-compliance review.
Related Posts
-
What Are the Types of Folding Cartons?
-
2026 Best Folding Carton Packaging Manufacturers
-

How to Choose the Right Folding Carton Styles for Your Packaging Needs
-
Top 10 Folding Carton Styles at the 139th Canton Fair?
-
Why Choosing the Right Folding Carton Styles is Crucial for Your Business Success
-
Top 10 Types of Folding Cartons You Need to Know for Your Packaging Solutions
